Material Transfer & Conveying
Bucket Elevator
for Bulk Materials
Ensure reliable and durable vertical conveying of bulk materials — up to 30 m lifting height and 50 t/h. Custom-designed bucket elevators built for demanding industrial environments.
VINCI Group / Actemium
30 Years of Bulk Handling Expertise
Up to 30 m Lifting Height
ATEX-Certified Design
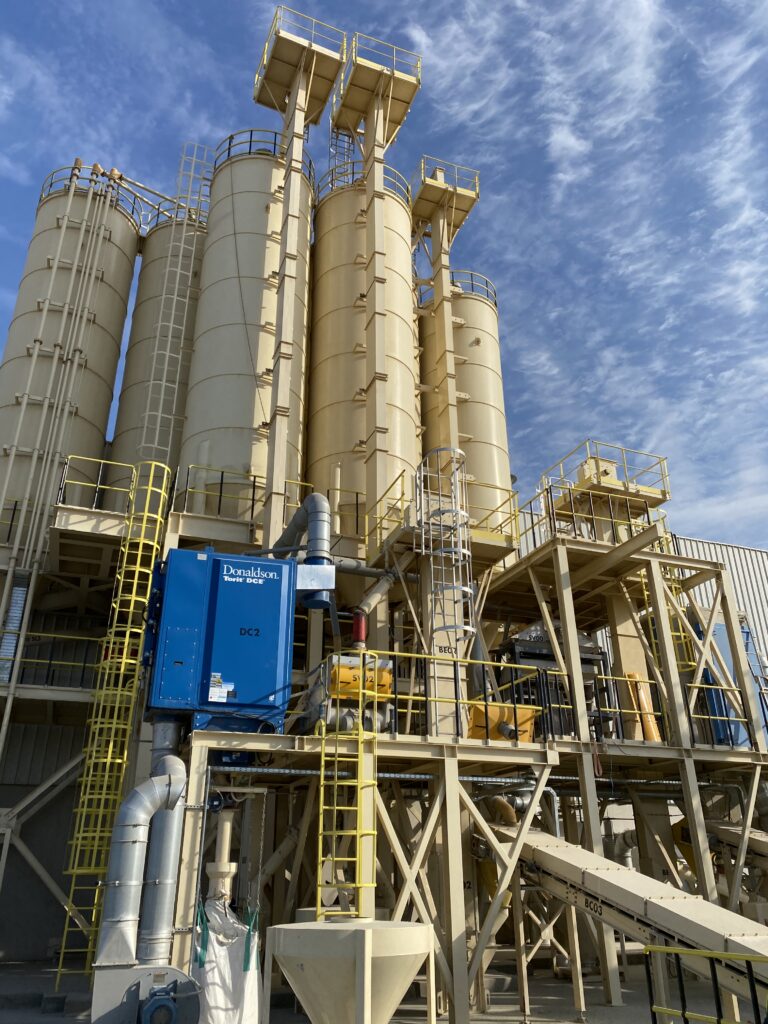
Our industrial bucket elevators provide reliable, efficient and durable vertical conveying of bulk materials. Suitable for many industries — chemicals, minerals and industrial powders — they handle your materials safely, even in demanding environments.
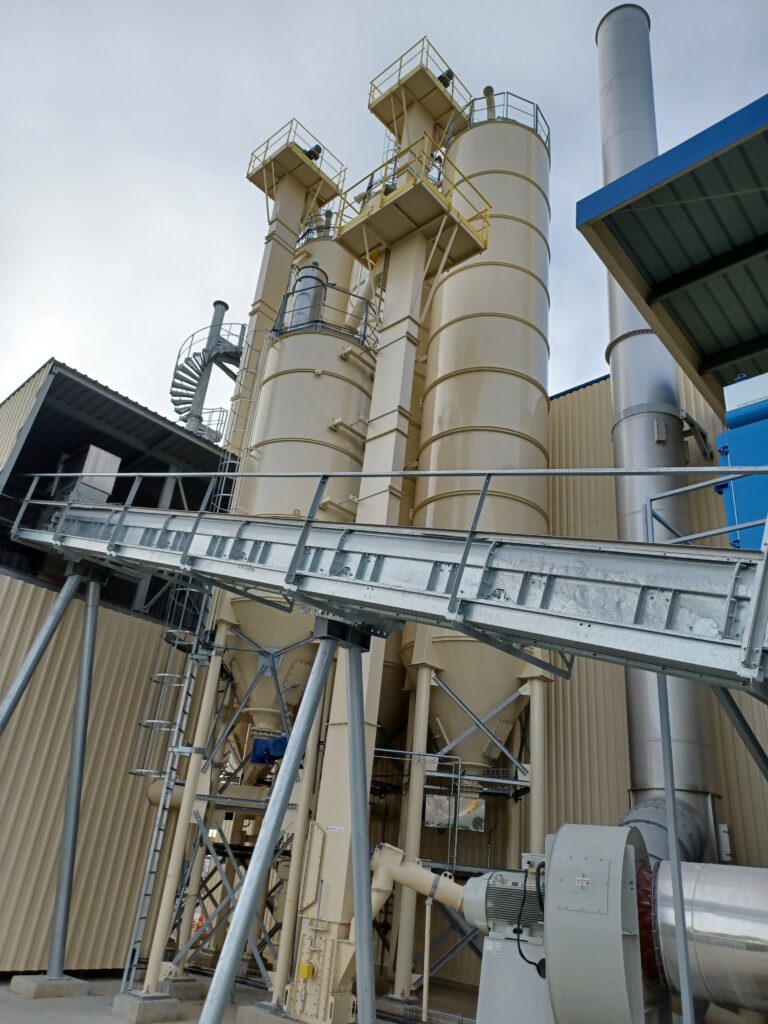
Sofraden Bulk offers a complete range of custom-designed bucket elevators, adaptable to every type of material, plant layout and production capacity.
Custom Engineering for Every Application
Each project is supported by an in-depth technical study to ensure optimal sizing:
- Selection of the belt and buckets to suit the conveyed material
- Selection of the elevator head to optimize performance
- Reduced installed power and lower process energy costs
- Integration into your industrial plant layout
Our modular design ensures a solution tailored to your process and production constraints.
Options for Your Bucket Elevator
A range of options and monitoring systems help keep your production safe.
Reinforcement & Access
- Heavy-Duty Version — for abrasive or aggressive materials
- ATEX-Certified Design — for potentially explosive areas
- Secure Access Doors — for inspection and cleaning
Monitoring & Operational Safety
- Speed monitoring
- Belt misalignment detection
- Blockage or overload sensors
- Real-time monitoring
Technical Specifications of Our Bucket Elevators
| Specification | Value |
|---|---|
| Conveying Capacity | Up to 50 t/h |
| Lifting Height | Up to 30 m |
| Installed Power | Up to 7.5 kW |
Robustness, Durability and Easier Maintenance
Backed by numerous installations worldwide, our technology delivers robust, durable equipment designed for continuous operation and reduced maintenance. Integrated self-supporting platforms provide easier access, with every detail designed to maximize your production line availability.
Continuous Operation
Low Maintenance
Self-Supporting Platforms
Applications of Our Bucket Elevators
Our elevators are used in production lines across various industries, including applications involving demanding bulk materials.
Industries: Chemicals · Minerals · Industrial powders
Applications: vertical conveying, continuous operation, demanding environments
Design Your Bucket Elevator with Sofraden Bulk
Engineering & Sizing
selection of the belt, buckets and elevator head to suit your material
Modular Design
tailored to your plant layout and capacity
Energy Optimization
reduced installed power
30 Years of Bulk Handling Expertise · After-Sales Service
Tell Us About Your Requirements. We’ll Size Your Bucket Elevator.
Lifting height, capacity, material characteristics and installation constraints: share your requirements and our team will get back to you with a technical assessment.
Frequently Asked Questions About Bucket Elevators
Up to 30 m lifting height and 50 t/h, with installed power of up to 7.5 kW.
Yes, an ATEX-certified design is available for potentially explosive atmospheres.
Yes, a dedicated heavy-duty version is available for these applications.
Through multiple monitoring systems: speed monitoring, belt misalignment detection, blockage or overload sensors and real-time monitoring.
Yes. Robust design keeps maintenance requirements low, while integrated self-supporting platforms and secure access doors make access easier.
Chemicals, minerals, industrial powders and, more broadly, demanding bulk-material handling environments.
Compliance
ATEX · CMR · FDA · EC 1935